

What to check on HD161 tires during incoming quality inspection
An incoming inspection for HD161 tires should not be limited to a visual check at the warehouse door. A tire can look new while carrying risks that only become apparent during mounting or early service: bead distortion from poor handling, sidewall cracking from storage exposure, specification mismatch, incomplete traceability, or a dimensional deviation that affects fitment and dual-tire operation.
The release decision should therefore answer two separate questions: does each tire conform to the approved specification, and has its condition remained suitable for safe installation since it left the factory? These are related but not interchangeable. A correctly manufactured tire can still be unacceptable if it has been mishandled, contaminated, or stored under damaging conditions.
Start with document and identity control
Before examining the physical tires, reconcile the shipment against the purchase order, approved technical data sheet, packing list, and any applicable regulatory or customer requirements. “HD161” is a commercial pattern or product identification, not a complete technical specification. The actual acceptance basis must include the ordered size, construction, ply rating or load range where applicable, load index, speed symbol, approved rim, quantity, and any required market markings.
Check that sidewall markings are legible, consistent, and appropriate to the order. At a minimum, the markings should identify:
- the HD161 designation or approved product identification;
- tire size and construction description;
- load and speed capability stated for the ordered specification;
- manufacturer identification and production date code;
- required conformity, approval, or regional markings for the destination market;
- tubeless or tube-type designation, where relevant; and
- any directional, axle-position, inflation, or mounting restrictions.
A common control failure is accepting tires on the basis of nominal size alone. Two tires may both be described as 11R22.5, for example, but have different load indexes, speed symbols, tread patterns, or intended service positions. The sidewall marking must match the approved release specification, not merely the broad size description on a carton label or shipping document.
Production-date control also deserves a defined internal rule. There is no universal incoming-receipt age limit that suits every jurisdiction, tire type, storage history, and fleet policy. What matters is that the date code is readable, the batch is traceable, the age is acceptable under the buyer’s written policy, and there is no evidence of adverse storage. A recent date code does not compensate for heat damage or ozone exposure; an older but properly stored tire should not be rejected solely on appearance without reference to the approved policy.
Inspect the tire in a way that reveals handling damage
Each tire should be rolled or rotated far enough to inspect the full circumference of both sidewalls, tread, shoulders, beads, inner liner, and any protective wrapping. Inspection under poor warehouse lighting is an avoidable source of escaped defects. Use clean, adequate lighting and keep sharp tools away from the tire surface.
Reject or quarantine tires showing cuts that expose cord, exposed or damaged bead wire, pronounced bead deformation, broken or displaced components, deep gouges, bulges, open splices, or evidence of impact. A bulge is particularly important because it can indicate separation or localized carcass damage beneath the rubber. It is not a cosmetic issue and should not be accepted on the assumption that inflation will restore the tire’s shape.
Surface conditions require judgment. Minor mold-release residue, superficial scuffs from normal handling, or light rubber bloom may not affect serviceability, but they should be distinguished from cracking, contamination, or structural injury. Petroleum products, solvents, grease, and certain cleaning chemicals can degrade rubber compounds or make a defect difficult to see. Tires with unknown chemical contamination should be isolated until the supplier provides an appropriate disposition.
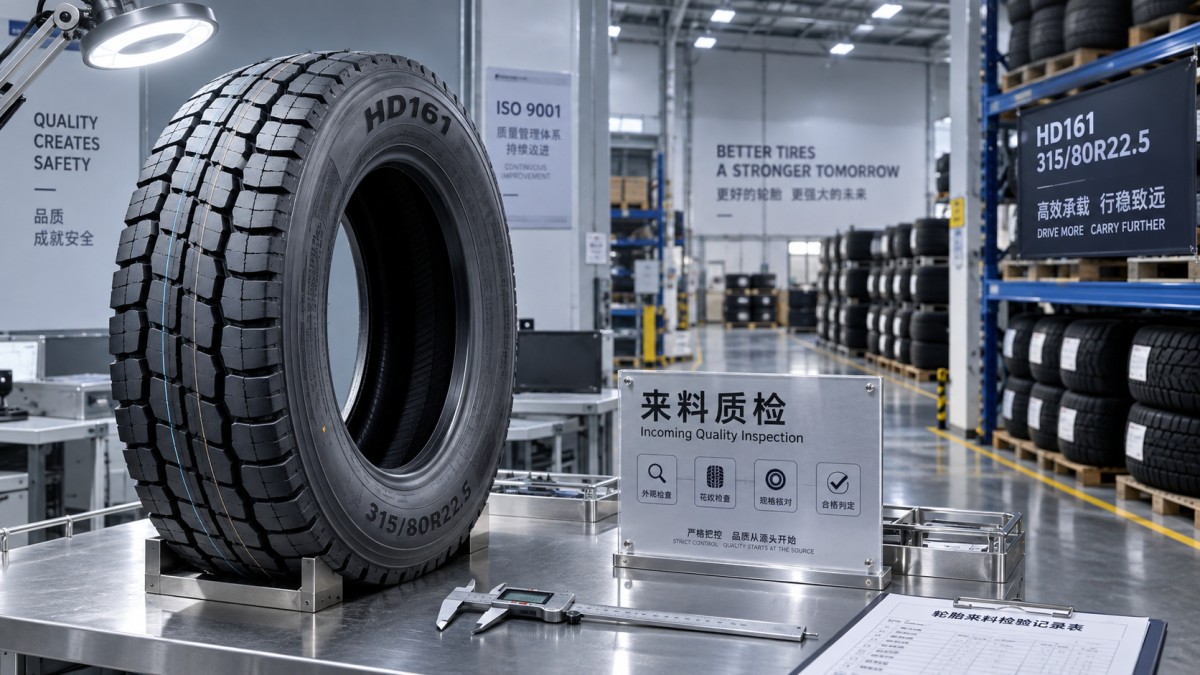
Pay close attention to the shoulder and sidewall transition. Forklift contact, excessive clamping, dragging over sharp edges, and incorrect stacking often leave damage in these areas. Sidewall abrasions may appear shallow but can become unacceptable if reinforcement cords are visible, if rubber has been removed to a significant depth, or if the damage is close to a flexing zone. Incoming personnel should not attempt cosmetic repair or trimming without a documented engineering disposition.
The bead area is the critical mounting interface
For tires intended for demanding truck service, bead condition deserves a dedicated inspection rather than a brief glance. The bead transfers mounting forces and helps establish the air seal on the rim. Damage can lead to inflation leaks, difficult seating, rim damage, or a mounting-related failure.
Inspect both beads for flattened sections, kinks, torn chafer material, wire exposure, cuts, cracking, contamination, and signs that the tire has been forced onto an unsuitable rim. The bead should retain a uniform circular profile. A tire that has been dropped, incorrectly stacked, or compressed under heavy loads can develop distortion that is easier to detect by rotating it on a clean inspection surface than by looking at it while it remains in a bundle.
The inner liner should also be clean and intact. For tubeless tires, liner cuts, folds, loose rubber, trapped packaging material, or embedded debris can compromise sealing. Do not use an inflated inspection to “prove” that a questionable bead is acceptable. Suspect tires should be held for supplier review or assessment under the manufacturer’s approved procedure.
Verify dimensions against the correct measurement condition
Dimensional inspection is valuable, but it is often performed incorrectly. Section width and overall diameter are not meaningful when measured on an unmounted, uninflated tire lying on a warehouse floor. Tire dimensions depend on the specified measuring rim, inflation condition, stabilization time, and the method defined by the applicable tire standard or manufacturer data.
Incoming checks should therefore be divided into two levels. At receipt, verify nominal dimensions, profile consistency, and obvious deformation using practical gauges or comparison fixtures. Formal dimensional verification should be conducted on a controlled sample basis using the approved standard rim and the manufacturer’s measurement procedure. The accepted tolerance must come from the applicable technical specification, not an arbitrary warehouse limit.
Tread depth should be checked at multiple locations across the crown, avoiding mold vents and local features that distort the reading. More important than one isolated depth value is consistency across the tire. Uneven tread depth on a new tire can indicate a molding issue, an incorrect product mixed into the shipment, or an unsuitable acceptance sample. Confirm that groove design, shoulder configuration, and tread pattern correspond to the approved HD161 reference.
Where a site handles several special-service patterns, pattern confusion is a real risk. For example, the specifications of HD182 include ST225/75R15 and ST235/80R16 sizes, each listed with a 9 mm tread depth. Those figures must never be used as an inspection criterion for HD161 tires. Pattern names, sizes, and tread-depth values are product-specific; inspectors should work only from the release sheet for the exact SKU received.
Traceability must allow containment, not just recordkeeping
A useful incoming record links every accepted tire, or at least every controlled batch, to the delivery note, purchase order, production date code, factory batch reference where supplied, inspection result, and storage location. This makes it possible to contain stock if a later issue affects a defined production period or shipment.
Record nonconformities with photographs, tire identification, quantity affected, defect location, and whether the issue is repeated across a batch. Vague entries such as “appearance problem” make later supplier investigation difficult. A precise description—such as “right bead chafer cut at approximately 70 mm, bead wire not visible”—creates a defensible basis for segregation and claim handling.
Sampling plans should reflect risk rather than convenience. A sealed shipment with stable supplier performance may justify a documented sampling approach for dimensions and detailed measurements, but identification, visible damage, and traceability checks still need sufficient coverage to prevent mixed specifications or transport damage from entering stock. If the same defect appears in more than one sampled unit, broaden the inspection rather than relying on the original sample size.
Storage findings can change the acceptance decision
Incoming inspection should include the condition of the delivery and receiving area. Tires stored near welding activity, electric motors that generate ozone, direct sunlight, heaters, standing water, oils, or solvents may deteriorate before installation. Check for wet packaging, compressed stacks, heat exposure, and deformation caused by excessive loading.
Tires should be segregated from questionable stock immediately and protected from further handling damage. The most effective receiving process is not one that identifies every possible defect; it is one that prevents an unresolved defect from being issued to a vehicle. Release only after the physical condition, marking conformity, dimensional status, and traceability record support the same conclusion: the HD161 tire received is the tire ordered, remains fit for mounting, and can be traced if a safety concern arises later.
Chat Online