

How to audit a passenger car tire manufacturer's traceability
Traceability Must Work in Both Directions
A traceability audit should answer two questions quickly and with evidence: can the manufacturer identify every input and process record behind a finished tire, and can it identify every finished tire affected by a suspect material, process setting, or test result? A system that can retrieve a production record from a tire's sidewall marking but cannot define the full affected population is incomplete for quality or recall control.
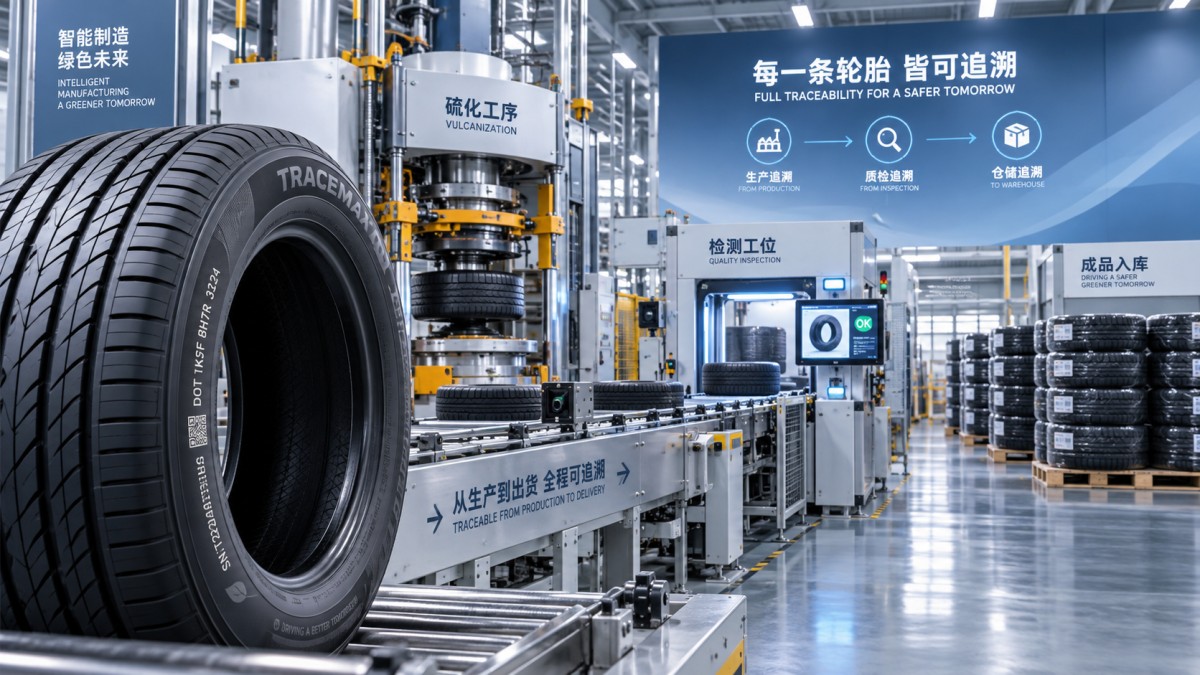
For a Passenger Car Tire Manufacturer, traceability is not simply a database exercise. The audit needs to show that the physical tire, the curing record, the component batches, the inspection result, and the shipment destination remain connected without relying on informal spreadsheet matching or individual staff knowledge.
Start by selecting several finished tires from different production dates, sizes, and customer shipments. Ask the factory to trace each sample backward. Then select a raw-material or component batch and ask it to trace forward. This two-way exercise reveals far more than a presentation of procedures and system screenshots.
Begin With the Tire Identity on the Shop Floor
The finished tire must carry an identifier that can be read reliably and linked to manufacturing records. Depending on the factory's system, this may be based on the serial number, DOT-style date code where applicable, barcode, RFID record, mold cavity information, or a controlled combination of these identifiers. The format itself matters less than its consistency and resistance to loss during production, storage, and shipment.
During the audit, follow the identifier from curing through final inspection, warehouse release, and dispatch. Look for manual relabelling, handwritten substitutions, unreadable codes, or points where tires are grouped into a batch without retaining unit-level linkage. These are common weak points because the production line may preserve a curing batch while the warehouse handles mixed pallets or partial shipments.
A useful test is to present the auditor-selected tire without advance notice and request the following records:
- Product specification, size, load index, speed symbol, and applicable construction code.
- Production order, production date or shift, machine and mold cavity where recorded.
- Curing cycle record and any associated alarm or deviation history.
- Final inspection and uniformity, balance, X-ray, or other test records required by the factory control plan.
- Release status, warehouse location, packing record, shipment document, and customer or destination reference.
Records should agree with one another. A traceability system can appear complete while containing mismatched dates, impossible routing sequences, or missing relationships between the production order and the shipping lot. Those inconsistencies matter because they expand the uncertainty of any containment action.
Audit the Inputs That Can Affect Tire Safety
Backward traceability should extend beyond a general recipe name. It should establish which controlled batches entered the tire and whether the manufacturer can distinguish approved material from material held for inspection or disposition.
For passenger car tires, the audit scope should normally cover the principal rubber compounds and reinforcing components used in the approved bill of materials: tread and sidewall compound batches, inner liner materials, textile or steel reinforcement where used, beads, chafer components, and curing bladders or other process-critical consumables when the factory defines them as traceability-relevant.
The goal is not to demand individual traceability for every minor item regardless of risk. The goal is to confirm that the manufacturer's traceability level matches its process risk analysis and recall capability. If a compound mixing batch is found to be out of specification, the factory should be able to identify the downstream components and finished tires made from it. If a reinforcement material is later linked to a supplier nonconformance, the factory should be able to isolate every affected production window.
Check the handoffs, not only the warehouse records
Material receipt records often look orderly because they are tied to supplier batch numbers. The more difficult audit point is the movement from stores to mixing, calendering, extrusion, component preparation, and tire building. Inspect how the factory prevents batch mix-up after materials have been opened, split, reworked, or transferred to line-side storage.
Ask how the system handles returned material, rework, partial rolls, and mixed remnants. A traceability process can become unreliable when an operator records only the original issue ticket but does not preserve the actual batch identity of material fed to the line. Physical labels, scanning discipline, segregation rules, and exception records should support the electronic trail.
Link Process Deviations to the Affected Tires
Many serious traceability gaps appear after a process deviation rather than at normal production. The audit should establish how the manufacturer records and evaluates events such as curing interruptions, temperature or pressure excursions, equipment alarms, component shortages, unplanned mold changes, inspection machine downtime, and nonconforming test results.
A reliable system identifies the precise time window, machine, cavity or station, and production sequence involved. It should also show whether the affected tires were blocked automatically, placed on hold, inspected at an increased level, reworked under authorization, or released through a documented concession process.
Do not accept a broad statement that “the shift was checked” as sufficient containment. Ask for one closed deviation record and compare it to actual production and warehouse data. The quantity initially contained, the quantity inspected, the quantity released, and the quantity scrapped or reclassified should reconcile. Where units have already shipped, the traceability record must identify the consignee and shipment route without delay.
This matters particularly for products intended for variable road conditions. For example, an all-terrain-oriented pattern such as AX380 may use tread features intended to support control and braking on mud roads while managing rolling resistance. Those design intentions do not reduce the need to trace compound, curing, and inspection history. A concern involving tread integrity or groove-area cracking must be containable by the actual tires and production conditions involved, not by a vague product-family label.
Test Recall Readiness With a Timed, Evidence-Based Exercise
A recall simulation is the strongest practical test of the system. Give the manufacturer a defined trigger, such as a component supplier batch, a mold cavity, a curing press, or a failed internal test result. Require it to produce an affected-tire list and show the evidence used to build it.
The exercise should be performed using normal systems and normal personnel, rather than a preassembled audit file. A fast answer is useful, but accuracy is more important than speed alone. The manufacturer should explain the logic used to define the affected population, including why adjacent production is included or excluded.
Look Beyond Certificates and Procedures
Certification and documented quality procedures can provide a management framework, but they do not prove that traceability works at the product level. Audit findings often arise from gaps between the written process and the production reality: scanners bypassed during high output, records completed after the shift, production identifiers reused, or warehouse transactions posted in batches long after physical movement.
Interview operators, inspectors, warehouse personnel, and quality staff separately. Their explanations of how a tire is identified, held, released, and shipped should be consistent. Observe whether the labels, work instructions, system terminals, and quarantine areas support those explanations.
Also verify retention and accessibility. Traceability data has little value if it cannot be retrieved after a system migration, staff change, or archival period. The factory should be able to demonstrate controlled backups, access permissions, correction rules, and an audit trail for changed records. A corrected record should retain its original context and approval history rather than silently replacing prior data.
Turn Findings Into a Practical Decision
Classify findings by their effect on containment. Missing formatting fields or inefficient report layouts may be correctable administrative issues. Inability to connect a finished tire to a component batch, an inspection decision, or a shipment destination is a higher-risk control failure. The latter should trigger a defined corrective-action plan before approving the manufacturer for safety-sensitive supply.
A credible traceability system leaves an evidence trail that survives routine production pressure and an unexpected quality event. When a Passenger Car Tire Manufacturer can trace backward to the relevant material and process history, forward to every affected shipment, and explain the boundaries of its result, quality and safety teams have a workable basis for supplier approval and recall readiness.
Chat Online